Unexpected breakdowns are costly, but servicing every machine too often can also waste time and money. Predictive maintenance offers a smarter middle path. It uses equipment condition and performance data to show when maintenance may actually be needed.
With predictive maintenance software, plant teams can spot warning signs, plan work earlier, and avoid unnecessary service.
What Is Predictive Maintenance?
Predictive maintenance is a maintenance approach that uses real equipment data to help predict when a machine may need attention.
Instead of servicing an asset only because a calendar date has arrived, teams look at its actual condition. This may include vibration, temperature, pressure, noise, oil condition, or other performance signals.
In simple terms, the predictive maintenance meaning is to maintain equipment when the data shows that a problem may be developing, rather than waiting for failure or servicing too early.
How Predictive Maintenance Works
Predictive maintenance software brings equipment data, condition trends, alerts, and maintenance information into one place.
Collect Equipment Condition Data
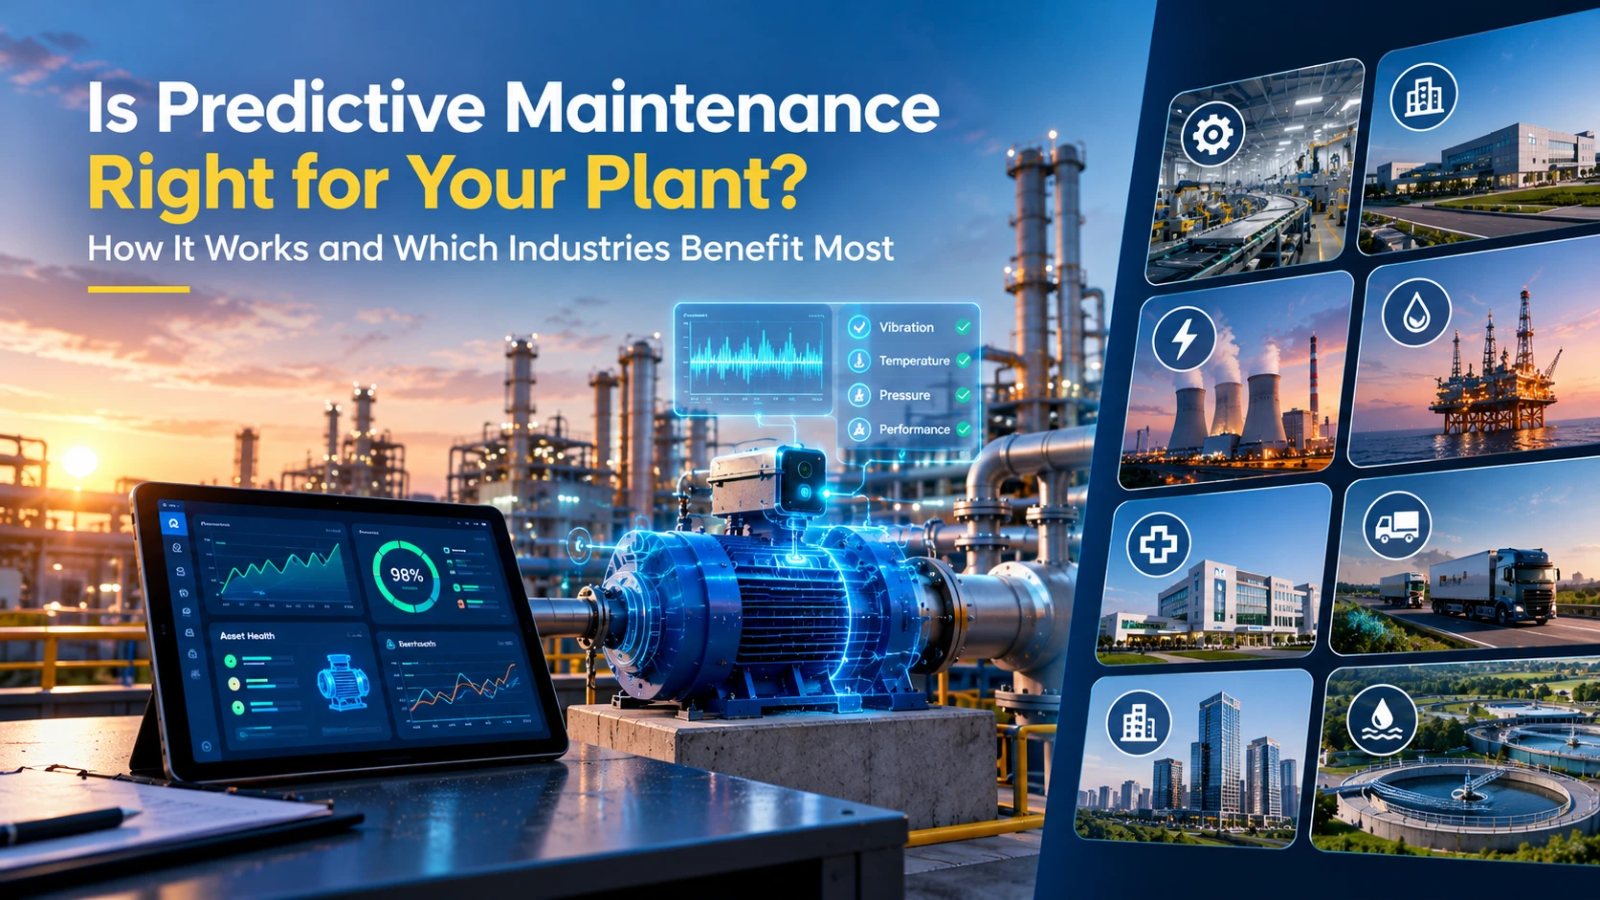
Sensors, machine controllers, inspections, or connected devices collect information about equipment health. For example, rising bearing vibration or motor temperature may point to early wear.
Identify Changes and Warning Signs
The system compares current readings with normal operating patterns. When values move outside expected limits, it can flag the change.
More advanced systems may also use historical data to identify patterns linked with past failures.
Turn Insights Into Maintenance Action
The goal is to act before a fault becomes a breakdown. A warning can be reviewed, prioritised, and converted into a maintenance task or work order.
What Are the Main Predictive Maintenance Benefits?
The biggest predictive maintenance benefits come from making maintenance more focused and timely.
Key advantages include:
- Reduced unplanned downtime
- Earlier detection of developing faults
- Better use of maintenance manpower
- Fewer unnecessary inspections or replacements
- Improved asset reliability
- Better spare-parts and shutdown planning
One of the main advantages of predictive maintenance is that teams can focus on machines showing real signs of deterioration instead of servicing every asset at the same fixed interval.
Is Predictive Maintenance Right for Every Plant?
Not always.
Predictive maintenance delivers the most value when equipment failure has a clear impact on production, safety, quality, or cost.
It may be a good fit when:
- Critical machines cause major production losses when they stop
- Equipment shows measurable signs before failure
- Emergency repairs are common
- The plant already collects useful condition data
- Fixed schedules lead to unnecessary maintenance
For simple, low-cost assets, traditional preventive maintenance may still be enough.
Which Industries Can Benefit From Predictive Maintenance?
Predictive maintenance software is especially useful where equipment reliability has a direct impact on output, quality, or plant availability.
Process and Continuous Manufacturing
Pharmaceutical, Chemicals, Food Processing, and FMCG plants often rely on pumps, mixers, compressors, conveyors, and filling lines.
Unexpected failures can disrupt batches or delay production. Condition monitoring can help teams spot early signs of wear and plan maintenance before a larger issue develops.
Discrete and High-Speed Manufacturing
Plastics & Polymer, Packaging & Printing, Automotive Components, and Electronics plants often operate high-speed or repetitive production equipment.
Moulding machines, presses, motors, printing lines, and assembly systems can create significant downtime when they stop unexpectedly. Predictive maintenance helps teams monitor critical assets and plan service around production windows.
Power and Renewable Energy
Power Plants and Renewable Energy operations depend on high-value equipment where reliability is essential.
Motors, turbines, generators, pumps, and gearboxes can benefit from vibration, temperature, and performance monitoring. The right software can help teams identify abnormal conditions earlier and plan work before failures affect availability.
Preventive vs Predictive Maintenance: What Is the Difference?
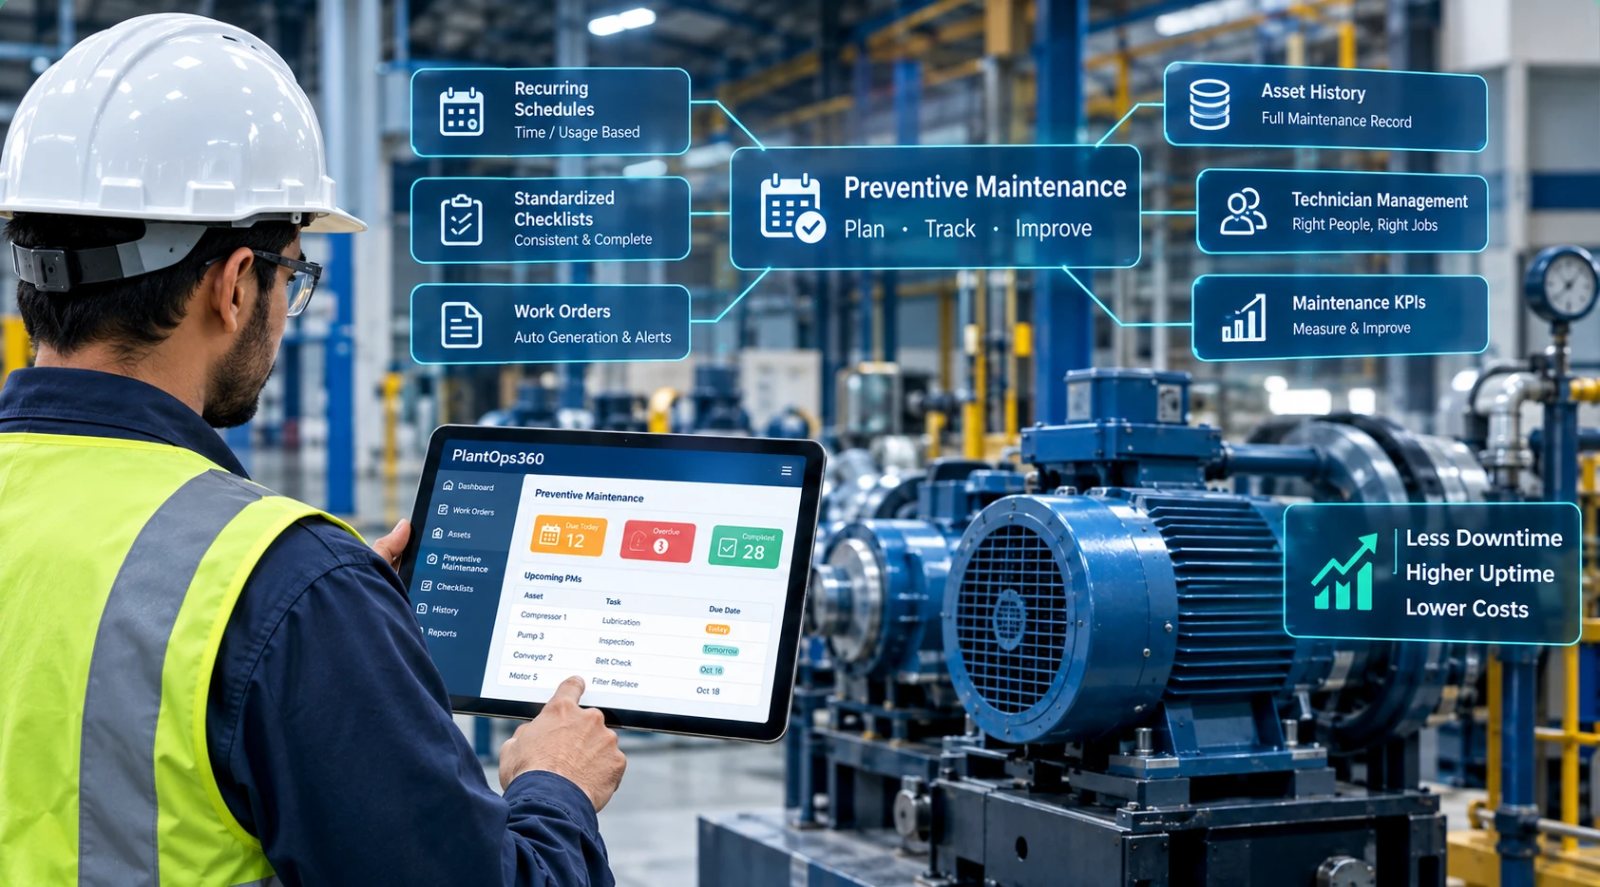
Preventive maintenance is performed at planned intervals, such as every month or every 500 operating hours.
Predictive maintenance is based on equipment condition. Maintenance is planned when data suggests performance is changing or a fault may be developing.
Many plants use both. Preventive maintenance works well for routine servicing, while predictive methods can add value for critical or condition-sensitive assets.
How to Start Predictive Maintenance Without Overcomplicating It
Start with a few critical assets where breakdowns are costly and equipment condition can be measured clearly.
Define what data matters, what counts as a warning, and what action should follow. Then track whether the approach reduces failures, improves planning, or avoids unnecessary work.
Once the process is working, the approach can be expanded to more assets, lines, or plant locations.
Frequently Asked Questions About Predictive Maintenance
Do you need sensors for predictive maintenance?
Not always. Sensors make continuous monitoring easier, but teams can also use inspection data, meter readings, oil analysis, or other condition information.
The right method depends on the equipment and the failure you want to detect.
How much historical data is needed before predictive maintenance becomes useful?
There is no fixed amount. Some condition limits can be used immediately, while advanced models usually improve as reliable operating and failure data becomes available.
Can predictive maintenance tools work with an existing CMMS or EAM system?
Yes, depending on the software. Integration can help convert equipment alerts into work orders and connect condition data with maintenance history and asset records.
Which assets should be selected first for predictive maintenance?
Start with assets that are critical, expensive to repair, difficult to replace, or known to create major downtime when they fail.
Conclusion
Predictive maintenance is most useful when plants need better control over critical equipment and have meaningful condition data to work with.
It can help teams detect developing problems earlier, plan work better, and reduce unnecessary maintenance. But it should be used where it makes operational and financial sense.
With predictive maintenance software, plant managers can turn condition data into clearer maintenance decisions. PlantOps360 can help teams build a more connected, data-driven maintenance process across pharmaceuticals, chemicals, food processing, FMCG, plastics and polymer, packaging and printing, automotive components, electronics, power, and renewable energy.